Glass Failures in Glass-lined Steel Equipment

Tom Patnaik

Share this article

G-force (bowl speed 1080 RPM at 48” diameter = 800 G’s)

Higher G’s accelerates filtration and deliquoring but increases attrition risk and can compress marginal cakes. Usually the G-force ranges from 800-1200.

Glass Failures in Glass-Lined Steel Process Equipment (Cliff Notes):

1. Purpose and Scope

  • This post aims to educate users about typical and atypical failures in glass-lined steel equipment, how to identify them, and preventive actions.
  • Failures are categorized as either typical (common, well-understood) or atypical (rare, often misunderstood and mysterious).

2. Typical Glass Failures

  • Mechanical Shock:
  • Accounts for ~75% of failures, often due to human error (e.g., improper handling, objects striking the vessel).
  • Prevention: Proper handling, training, and maintenance procedures.
  • Corrosion:
  • Glass is not completely inert; acids, alkalis, and water can corrode glass.
  • Acid Attack: Most acids are resisted except hydrofluoric acid and some concentrated acids at high temperatures.
  • Hydrofluoric Acid/Fluoride Impurities: Even low concentrations can rapidly destroy glass; vigilance and chemical analysis are required.
  • Alkaline Attack: More severe than acid; increases with concentration and temperature.
  • Water Vapor Attack: Pure water, especially as vapor, can cause significant corrosion.
  • Prevention: Monitor chemical concentrations and temperatures, and follow manufacturer corrosion charts.
  • Abrasion:
  • Caused by abrasive solids; rare alone but severe when combined with corrosion.
  • Prevention: Use of protective boots on agitators/baffles, improved glass formulations.
  • Thermal Shock and Stress:
  • Sudden temperature changes can cause glass to fracture.
  • Prevention: Adhere to safe temperature differentials, gradual heating/cooling, and use of temperature sensors.
  • Overstressing Nozzles:
  • Excessive torque or piping stress can fracture glass at nozzles.
  • Prevention: Follow torque specs, use expansion joints, and proper support.
  • Metal Repair Failure:
  • Improper installation or material choice (e.g., tantalum plugs) can lead to leaks and further damage.
  • Prevention: Correct installation, periodic inspection, and use of proper cements.
  • Miscellaneous Failures:
  • Excess pressure/vacuum, point impingement, improper vessel support, gasket failure, excessive agitator torque, and baffle tip failure.
  • Prevention: Routine maintenance, correct installation, and operational vigilance.

3. Atypical Glass Failures

  • Ladder Type Failure:
  • Horizontal cracks below jacket overflow, often due to vacuum siphoning coolant into the jacket.
  • Prevention: Use vacuum breakers and positive shutoff valves.
  • Electrostatic Discharge Failure:
  • Static buildup from immiscible liquids/agitation can puncture glass.
  • Prevention: Make reagents conductive, reduce agitation, avoid free-falling liquids, inert gas purging, use conductive glass lining
  • Nascent Hydrogen Attack:
  • Acid on steel forms hydrogen ions, which diffuse through the metal, collect beneath the glass, and expand 5X when they come together to form a molecule, thereby fracturing the glass.
  • Prevention: Immediate neutralization and cleaning of acid spills.
  • Cavitation:
  • Gas bubbles imploding at agitator/baffle blades cause chipping.
  • Prevention: Avoid low-level agitation and direct gas injection with large bubbles.
  • Other Rare Failures:
  • Aluminum chloride reactions, spark testing, alkyl chloride reactions, freezing of water in baffles stored outdoors.
  • Prevention: Specific operational controls and testing.

4. Flaw Detection and Monitoring

  • Early detection is critical; systems are available from the major glass-steel equipment manufacturers that can identify flaws before major failure.
  • Regular inspections and adherence to manufacturer guidelines.

5. Conclusion

  • Proper care, common sense, and understanding of equipment limitations are essential.
  • Real-world failures may involve multiple interacting variables.

Example Implementation:

  • Training: Ensure all operators are trained in proper handling and maintenance procedures.
  • Maintenance: Schedule regular inspections, especially after suspected mechanical or thermal shock.
  • Chemical Analysis: Test all reactants for fluoride impurities before use.
  • Operational Controls: Use temperature sensors and adhere to safe temperature differentials.
  • Repair Protocols: Use only manufacturer-approved materials and methods for repairs.

If you would like us to come in and discuss how you can get more life out of your old glass-lined steel reactors, please contact us.


Share this article

Recent Posts

The 4 Forces Driving Pharmaceutical Barrier Systems to the Next Generation
By Tom Patnaik • October 16, 2026
Discover the four key market and technology forces driving the evolution of next-generation pharmaceutical barrier systems and manufacturing safety.
By Tom Patnaik • September 25, 2026
How Two Pharma Revolutions Are Really One Story. For most of the twentieth century, a pharmaceutical capital equipment sale had a predictable shape. A customer needed a glass-lined reactor, and the sweet spot — the size that made economic sense for a new API production line — sat comfortably at 2,000 to 3,000 (maybe 4,000) gallons. That assumption held for decades. For pharmaceutical API production specifically, it doesn't hold true anymore. Today, when a pharmaceutical customer specs a new glass-lined reactor project — particularly one built around a highly potent compound — it's increasingly landing at under half that, or just about ~1,000 gallons, or less. The 2,000–3,000-gallon vessels that once defined the category are still being bought for pharma applications too, but mostly as replacements for equipment installed 40 or 50 years ago, not as the standard for new capacity. This isn't a universal shrinkage across every glass-lined reactor application, though: greenfield agrochemical and other specialty chemical projects, where the chemistry is typically bulk and non-potent, still routinely spec vessels at 2,000, 3,000, even 6,000 gallons, because scale economics still favor size when high-potency and containment aren't the driving constraint. The story here is specific to pharma, and more specifically to the high-potency-driven end of it. Having sold into these accounts for decades, I've watched the pharma sweet spot shrink in real time, and I've come to believe it's not really a story about reactor size at all. It's a story about potency, precision, and the shape of the pharmaceutical market itself — and it's a story that's now repeating, almost beat for beat, a generation later, in an entirely different part of the industry: biologics manufacturing.
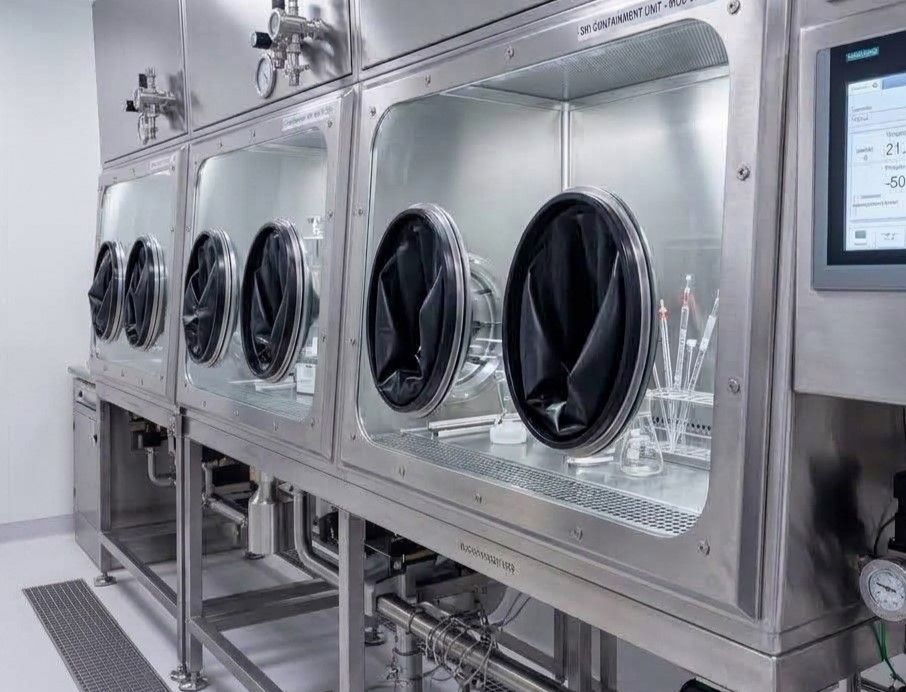
Flex Single-Use Isolators, Robotic Arms, and PAT: Are We Entering a 5th Generation of Barrier Techno
By Tom Patnaik • September 21, 2026
Explore the evolution of pharmaceutical barrier technology from 1st-gen RABS to 5th-gen single-use flexible isolators, robotics, and integrated PAT systems.